6 kW fiber laser cutting chart for brass

Updated:

Short answer

At 6 kW the chart cuts brass from 1 to 20 mm: with nitrogen for 1–12 mm, with nitrogen or air for 16–20 mm. Speed runs from 30–40 m/min at 1 mm down to 0.15 m/min at 20 mm.

Cutting speed and gas pressure by thickness

ThicknessGasPressure, bar Speed, m/minPower, % Gas per 1 mFocus, mmHeight, mmNozzle
1 mm N₂1230–40100
2 mm N₂1218–20100
3 mm N₂1412–14100
4 mm N₂148–9100
5 mm N₂145–5.5100
6 mm N₂163.2–3.8100
8 mm N₂161.5–1.8100
10 mm N₂160.8–1100
12 mm N₂180.6–0.7100
16 mm N₂ / air160.35100
20 mm N₂ / air160.15100

Brass cutting at different power: what each kilowatt gives

Thickness 3 kW, m/min6 kW, m/min12 kW, m/min
1 mm 20–2830–4035–45
2 mm 10–1518–2030–35
3 mm 5–612–1418–22
4 mm 2.5–38–915–18
5 mm 1.8–2.25–5.512–15
6 mm 0.8–13.2–3.88–10

At 4 mm, going from 6 kW to 12 kW cuts about 1.9 times faster.

Common brass cutting defects
Burn-through on the reverse side of brass
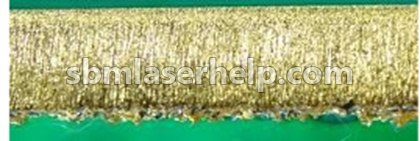
Burn-through on the reverse side of brass Metal tearouts and large droplets on the reverse side of the brass sheet. Cause: Assist gas pressure too low, power too high at feed rate too low. First step: Increase the assist gas pressure (step 1 bar). Where should the focus sit for stainless steel and mild steel?
Roughness on the bottom edge of brass
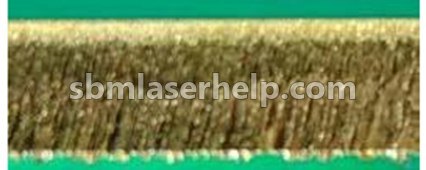
Roughness on the bottom edge of brass Pronounced striation and roughness in the lower portion of the brass part kerf. Cause: Focus position too high, gas pressure too high. First step: Raise the focus (step 0.5 mm). Why is the cut edge rough and striated instead of smooth?
Beam reflection / Cut interruption on brass
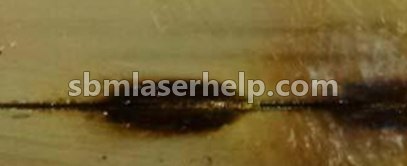
Beam reflection / Cut interruption on brass The beam reflects off the mirror surface of brass, no through kerf is produced. Cause: High reflectivity of the alloy, feed rate too high. First step: Reduce the speed (step 5%). Fiber laser stopped cutting through the sheet — what is wrong?

Not sure which one you have? Send a photo of the edge to the app and it names the defect and the fix.

Brass cutting charts at other power

Related questions

How thick brass can a 6 kW fiber laser cut?
The chart goes up to 20 mm, with nitrogen or air, at 0.15 m/min.
Which gas to cut brass with at 6 kW?
By the chart: with nitrogen for 1–12 mm, with nitrogen or air for 16–20 mm. The app picks the exact mode for your machine and nozzle.
Where are focus, nozzle and cutting height?
For every row of the chart they are in the SBM Laser Help app, together with alternative modes from other sources.

Ranges are given for a typical 3–6 kW fiber machine with a clean beam path. Always verify against your machine manufacturer’s table before production.

Need the numbers for your exact machine?

See what is inside

SBM Laser Help carries cutting and piercing parameter tables by material, thickness and gas, photo diagnosis of cut defects, machine and chiller error codes, and gas consumption calculators. Free account, no card.