Cutting brass on a fiber laser
Brass reflects most of the fiber laser beam and pulls heat away from the cut, so it is cut with high-pressure nitrogen or air and needs a power margin. On thicker sheet the beam can bounce off the surface and the cut breaks off. Cutting parameters by power and thickness are listed below; focus, cutting height and nozzle for each are in SBM Laser Help.
All cutting modes by metal, thickness, gas and laser power, with alternative modes, are in the SBM Laser Help parameter tables.Parameter tables in the app →
Fiber laser settings for brass by power and thickness
Common brass cutting defects
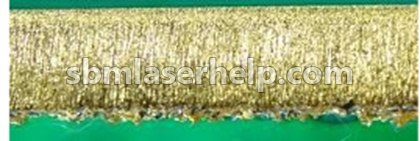
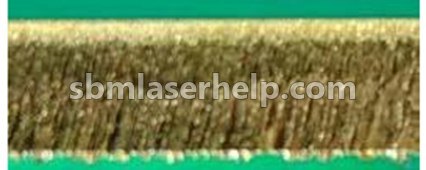
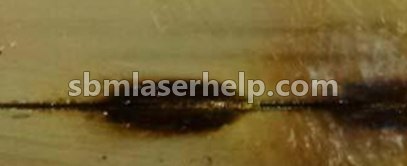
Cut quality problems
- Fiber laser stopped cutting through the sheet — what is wrong?
When a machine that used to cut through stops penetrating, the beam is losing energy on its way to the sheet or landing in the wrong place. In order of likelihood: dirty or cracked protective glass, worn nozzle, focus drift, gas pressure loss, and only then the source itself.
Read the answer → - Why is the cut edge rough and striated instead of smooth?
Striations are the fingerprint of an unstable melt front. Coarse, dragging lines mean the melt cannot keep up — usually speed, focus or gas dynamics. Fine even lines are normal and cannot be removed entirely; what you control is their depth and how far down the edge they start.
Read the answer → - Why does my laser cutter throw spatter and clog the nozzle?
Spatter is melt ejected back up toward the head instead of down through the kerf — usually from piercing thick material too aggressively, standoff set too low, or pressure too high for the nozzle. It clogs the nozzle fast, and a clogged nozzle then makes spatter worse.
Read the answer → - Why is my laser-cut kerf tapered — wider at the top than the bottom?
Taper means the beam is not delivering a straight-walled cut through the full thickness: usually focus sitting at or above the surface on thick material, speed slightly too high, or a worn lens spreading the beam. It shows up mostly on plate over 8–10 mm, where the beam has more depth to travel through.
Read the answer →


