3 kW fiber laser cutting chart for aluminium

Updated:

Short answer

At 3 kW the chart cuts aluminium from 1 to 10 mm: with nitrogen for 1–8 mm, with nitrogen or air for 7–10 mm. Speed runs from 25–30 m/min at 1 mm down to 0.4 m/min at 10 mm. Thicker plate needs 6 kW, up to 20 mm.

Cutting speed and gas pressure by thickness

ThicknessGasPressure, bar Speed, m/minPower, % Gas per 1 mFocus, mmHeight, mmNozzle
1 mm N₂1225–30100
2 mm N₂1215–18100
3 mm N₂147–8100
4 mm N₂145–6100
5 mm N₂162.5–3100
6 mm N₂161.5–2100
7 mm N₂ / air160.3100
8 mm N₂160.6–0.7100
10 mm N₂ / air160.4100

Aluminium cutting at different power: what each kilowatt gives

Thickness 3 kW, m/min6 kW, m/min12 kW, m/min
1 mm 25–3030–4545–50
2 mm 15–1820–2530–35
4 mm 5–68–1018–20
5 mm 2.5–35–614–16
8 mm 0.6–0.71.5–26–8
10 mm 0.41–1.24–6

At 5 mm, going from 3 kW to 6 kW cuts about 2 times faster.

Common aluminium cutting defects
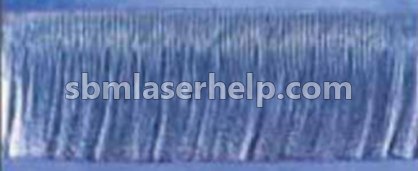
Severe striation curl (Bottom waviness)
Severe striation curl (Bottom waviness) Pronounced lag of drag lines in the lower portion of the cut (beam lag), resulting in a rough dross. Cause: Speed too high, power too low, focus too deep, assist gas pressure too low. First step: Decrease the speed (step 5%). Why is the cut edge rough and striated instead of smooth?
Porous dross along the sides
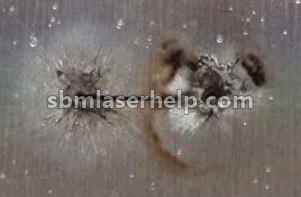
Porous dross along the sides Adhesion of loose, porous aluminum dross along the bottom edge. Cause: Focus set too deep, cutting speed set too high. First step: Raise the focus (step 0.5 mm). What settings does laser cutting aluminium need?
Incomplete cut on aluminum / Beam loss
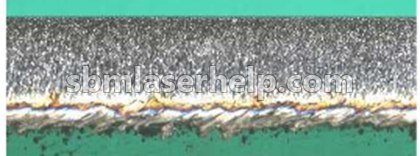
Incomplete cut on aluminum / Beam loss The beam breaks down, forming an uncut groove with foamed aluminum melt. Cause: Feed rate too high, focus too low, assist gas pressure excessive. First step: Reduce the speed (step 5%). Fiber laser stopped cutting through the sheet — what is wrong?

Not sure which one you have? Send a photo of the edge to the app and it names the defect and the fix.

Aluminium cutting charts at other power

Related questions

How thick aluminium can a 3 kW fiber laser cut?
The chart goes up to 10 mm, with nitrogen or air, at 0.4 m/min. Thicker plate is cut at 6 kW.
Which gas to cut aluminium with at 3 kW?
By the chart: with nitrogen for 1–8 mm, with nitrogen or air for 7–10 mm. The app picks the exact mode for your machine and nozzle.
Where are focus, nozzle and cutting height?
For every row of the chart they are in the SBM Laser Help app, together with alternative modes from other sources.

Ranges are given for a typical 3–6 kW fiber machine with a clean beam path. Always verify against your machine manufacturer’s table before production.

Need the numbers for your exact machine?

See what is inside

SBM Laser Help carries cutting and piercing parameter tables by material, thickness and gas, photo diagnosis of cut defects, machine and chiller error codes, and gas consumption calculators. Free account, no card.