Fiber laser settings for 3 mm mild steel at 3 kW
Updated:
A 3 kW fiber laser cuts 3 mm mild steel with oxygen at 0.5–0.8 bar and 2.04–4 m/min or with air at 3.9–20 bar and 7.7–12 m/min. For this combination we have 11 regimes: the base one from the source maker’s table and 10 alternatives from other sources.
Mild steel cutting speed and gas pressure at 3 kW
Which regime to start with
- Base regime. The starting point for most 3 kW machines, from the source maker’s own table.
- Alternative 1. Faster: 10 m/min against 3.2–3.6 m/min. Gas pressure 11.4 bar higher. Source: MAX, Head: none. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 2. Faster: 7.7 m/min against 3.2–3.6 m/min. Gas pressure 19.4 bar higher. Source: MAX, Head: Precitec. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 3. Faster: 8 m/min against 3.2–3.6 m/min. Gas pressure 3.3 bar higher. Source: GW, Head: ECA740SS. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 4. Faster: 12 m/min against 3.2–3.6 m/min. Gas pressure 11.4 bar higher. Source: MAX, Head: Raytools bm111. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 5. Faster: 8 m/min against 3.2–3.6 m/min. Gas pressure 15.4 bar higher. Source: MAX 3000W, Head: OSPRI. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 6. Faster: 3.6 m/min against 3.2–3.6 m/min. Oxygen pressure 0.2 bar higher. Source: MAX MFSC-3000X-50um, Head: none. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 7. Faster: 4 m/min against 3.2–3.6 m/min. Oxygen pressure 0.1 bar lower. Source: MAX, Head: none. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 8. Faster: 3.6 m/min against 3.2–3.6 m/min. Source: Raycus, Head: Raytools bm111. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
- Alternative 9. Slower: 2.04 m/min against 3.2–3.6 m/min. Source: Raycus, Head: none. Try it on a rusty or scaled sheet, or when the base regime does not cut through cleanly.
- Alternative 10. Faster: 3.9 m/min against 3.2–3.6 m/min. Oxygen pressure 0.1 bar higher. Source: Raycus, Head: Raytools. Try it when the cut is clean and you want more speed; if the edge gets worse, go back to the base regime.
Cutting time and gas consumption per metre
At these speeds one metre of cut takes about 5–29 seconds. Oxygen flow through the nozzle is about 0.9–3.4 m³ per hour, or 4–27 litres per metre of cut, not counting piercing. Air flow through the nozzle is about 6.3–190.5 m³ per hour, or 13–412 litres per metre of cut, not counting piercing.
Mild steel cutting speed chart: neighbouring thickness and power
| Thickness · power | Gas | Speed, m/min |
|---|---|---|
| 1 mm · 3 kW | N₂ / air | 28–35 |
| 2 mm · 3 kW | N₂ / air | 16–20 |
| 2 mm · 3 kW | O₂ | 3.8–4.2 |
| 3 mm · 2 kW | O₂ | 4.2 |
| 3 mm · 3 kW | O₂ | 3.2–3.6 |
| 3 mm · 4 kW | N₂ / air | 8–12 |
| 3 mm · 4 kW | O₂ | 4–4.5 |
| 3 mm · 6 kW | N₂ / air | 12–14 |
| 3 mm · 6 kW | O₂ | 3.5–4.2 |
| 4 mm · 3 kW | O₂ | 3–3.2 |
| 5 mm · 3 kW | O₂ | 2.7–3 |
Going from 3 kW to 4 kW gives about 25% more speed on 3 mm with oxygen. Nitrogen or air cuts about 2.9 times as fast as oxygen here, but needs 4 kW.
Common mild steel cutting defects with oxygen and with air
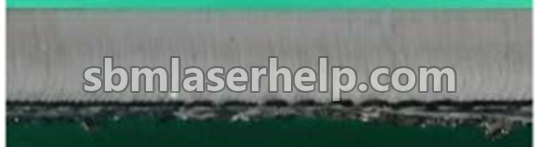
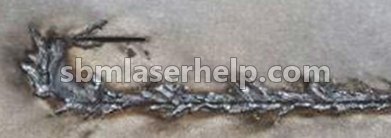
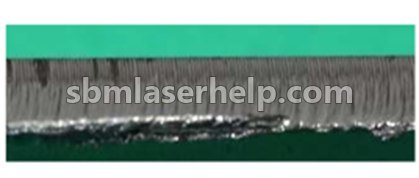
Not sure which one you have? Send a photo of the edge to the app and it names the defect and the fix.
Related questions
- What is the thickest mild steel a 3 kW fiber laser cuts?
- Our tables go up to 26 mm mild steel at 3 kW, at 0.23 m/min with oxygen. The next thickness, 30 mm, starts from 8 kW.
- Why is the speed a range?
- Sheet surface, mild steel grade, oxygen purity and the state of the protective window all shift the result. Start at the lower value, make a test cut and raise the speed in 5% steps while the bottom edge stays clean.
- Where are focus, cutting height and nozzle?
- They depend on the cutting head and lens, so a single number is often wrong for your machine. The app shows the full regime and fits it to the machine you add to your profile.