3 kW fiber laser cutting chart for mild steel
Updated:
Short answer
At 3 kW the chart cuts mild steel from 1 to 26 mm: with nitrogen or air for 1–2 mm, with oxygen for 2–26 mm. Speed runs from 28–35 m/min at 1 mm down to 0.23 m/min at 26 mm.
Cutting speed and gas pressure by thickness
| Thickness | Gas | Pressure, bar | Speed, m/min | Power, % | Gas per 1 m | Focus, mm | Height, mm | Nozzle |
|---|---|---|---|---|---|---|---|---|
| 1 mm | N₂ / air | 10 | 28–35 | 100 | ||||
| 2 mm | N₂ / air | 10 | 16–20 | 100 | ||||
| O₂ | 1.6 | 3.8–4.2 | 70 | |||||
| 3 mm | O₂ | 0.6 | 3.2–3.6 | 70 | ||||
| 4 mm | O₂ | 0.6 | 3–3.2 | 80 | ||||
| 5 mm | O₂ | 0.6 | 2.7–3 | 100 | ||||
| 6 mm | O₂ | 0.6 | 2.2–2.5 | 100 | ||||
| 7 mm | O₂ | 0.52 | 2.2 | 90 | ||||
| 8 mm | O₂ | 0.6 | 1.8–2.2 | 100 | ||||
| 10 mm | O₂ | 0.6 | 1–1.3 | 100 | ||||
| 11 mm | O₂ | 0.6 | 0.55 | 80 | ||||
| 12 mm | O₂ | 0.6 | 0.9–1 | 80 | ||||
| 14 mm | O₂ | 0.6 | 0.8–0.9 | 80 | ||||
| 15 mm | O₂ | 0.65 | 0.8 | 55 | ||||
| 16 mm | O₂ | 0.6 | 0.6–0.7 | 80 | ||||
| 18 mm | O₂ | 0.6 | 0.5–0.6 | 80 | ||||
| 20 mm | O₂ | 0.6 | 0.4–0.55 | 80 | ||||
| 22 mm | O₂ | 0.6 | 0.45–0.5 | 80 | ||||
| 25 mm | O₂ | 0.8 | 0.54 | 100 | ||||
| 26 mm | O₂ | 0.8 | 0.23 | 90 |
Mild steel cutting at different power: what each kilowatt gives
| Thickness | 3 kW, m/min | 6 kW, m/min | 12 kW, m/min |
|---|---|---|---|
| 1 mm | 28–35 | 35–45 | 50–60 |
| 4 mm | 3–3.2 | 8–10 | 20–24 |
| 8 mm | 1.8–2.2 | 2.2–2.5 | 7–10 |
| 12 mm | 0.9–1 | 1.9–2.1 | 1.8–2 |
| 18 mm | 0.5–0.6 | 0.8 | 1.6 |
| 25 mm | 0.54 | 0.5 | 0.8–1 |
At 12 mm, going from 3 kW to 6 kW cuts about 2.1 times faster.
Common mild steel cutting defects
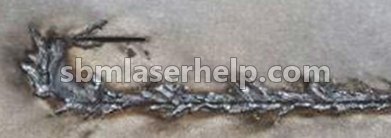
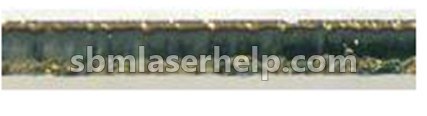
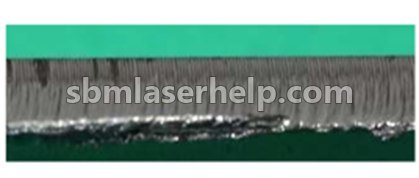
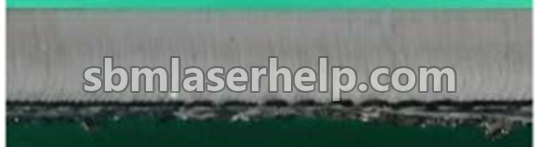
Not sure which one you have? Send a photo of the edge to the app and it names the defect and the fix.
Mild steel cutting charts at other power
Related questions
- How thick mild steel can a 3 kW fiber laser cut?
- The chart goes up to 26 mm, with oxygen, at 0.23 m/min.
- Which gas to cut mild steel with at 3 kW?
- By the chart: with nitrogen or air for 1–2 mm, with oxygen for 2–26 mm. The app picks the exact mode for your machine and nozzle.
- Where are focus, nozzle and cutting height?
- For every row of the chart they are in the SBM Laser Help app, together with alternative modes from other sources.