6 kW fiber laser cutting chart for stainless steel
Updated:
Short answer
At 6 kW the chart cuts stainless steel from 1 to 25 mm: with nitrogen for 1–20 mm, with nitrogen or air for 22–25 mm. Speed runs from 40–50 m/min at 1 mm down to 0.15 m/min at 25 mm. Thicker plate needs 12 kW, up to 40 mm.
Cutting speed and gas pressure by thickness
Swipe the table sideways →
Thickness
Gas
Pressure, bar
Speed, m/min
Power, %
Gas per 1 m
Focus, mm
Height, mm
Nozzle
1 mm
N₂
10
40–50
100
2 mm
N₂
12
25–30
100
3 mm
N₂
12
15–18
100
4 mm
N₂
14
10–12
100
5 mm
N₂
14
7–8
100
6 mm
N₂
15
6–7
100
8 mm
N₂
15
3.5–3.8
100
10 mm
N₂
15
1.6–2
100
12 mm
N₂
16
1–1.2
100
14 mm
N₂
16
0.8–1
100
16 mm
N₂
18
0.5–0.6
100
18 mm
N₂
20
0.4–0.5
100
20 mm
N₂
20
0.2–0.35
100
22 mm
N₂ / air
16
0.45
100
25 mm
N₂ / air
16
0.15
100
Stainless steel cutting at different power: what each kilowatt gives
Thickness
3 kW, m/min
6 kW, m/min
12 kW, m/min
1 mm
28–35
40–50
50–60
3 mm
7–10
15–18
30–35
4 mm
5–6.5
10–12
22–28
6 mm
2–2.7
6–7
14–17
8 mm
1–1.2
3.5–3.8
9–11
16 mm
0.3
0.5–0.6
2.2–2.4
At 6 mm, going from 6 kW to 12 kW cuts about 2.4 times faster.
Common stainless steel cutting defects
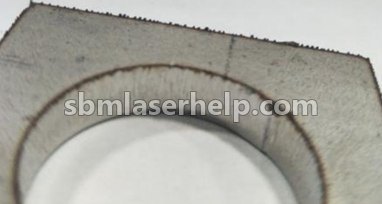
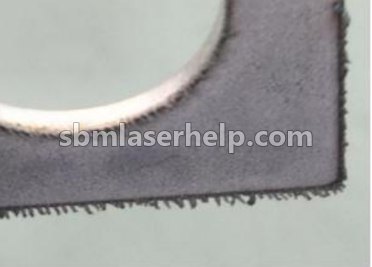
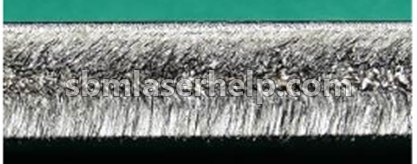
Needle-like (fine) drossFine needle-like burr along the full length of the bottom edge, easily removed.Cause: Cutting speed too high, focus set too deep.First step: Raise the focus (step 0.5 mm).Why does a fiber laser leave burr on stainless steel?
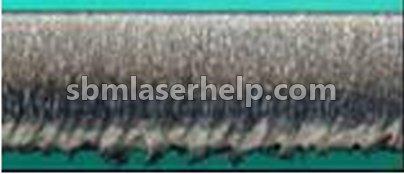
Long thick drossHeavy, massive drops and 'icicles' of solidified metal on the bottom edge.Cause: Insufficient nitrogen/air pressure, excessive speed, buried focus.First step: Raise the focus (step 0.5 mm).Why does a fiber laser leave burr on stainless steel?
Plasma formation (Plasma cloud)Bright blue/violet glow above the cutting zone, reduction in beam penetration, melting of the top edge.Cause: Insufficient nitrogen pressure, cutting speed too high or power set too high.First step: Increase the nitrogen assist gas pressure (step 1 bar).Where should the focus sit for stainless steel and mild steel?
Bottom edge melting and darkeningThe bottom portion of the edge has a dark blue/brown color (oxidation) with visible signs of overheating.Cause: Low nitrogen pressure, insufficient gas flow to cool the kerf zone.First step: Increase the nitrogen assist gas pressure (step 1 bar).Why does a fiber laser leave burr on stainless steel?
Not sure which one you have? Send a photo of the edge to the app and it names the defect and the fix.
How thick stainless steel can a 6 kW fiber laser cut?
The chart goes up to 25 mm, with nitrogen or air, at 0.15 m/min. Thicker plate is cut at 12 kW.
Which gas to cut stainless steel with at 6 kW?
By the chart: with nitrogen for 1–20 mm, with nitrogen or air for 22–25 mm. The app picks the exact mode for your machine and nozzle.
Where are focus, nozzle and cutting height?
For every row of the chart they are in the SBM Laser Help app, together with alternative modes from other sources.
Ranges are given for a typical 3–6 kW fiber machine with a clean beam path. Always verify against your machine manufacturer’s table before production.
Need the numbers for your exact machine?
See what is inside
SBM Laser Help carries cutting and piercing parameter tables by material, thickness and gas, photo diagnosis of cut defects, machine and chiller error codes, and gas consumption calculators. Free account, no card.